By Michael Nielsen, Publisher | 15+ Years in Diesel Repair
Last Updated: September 2026
⏱ Estimated reading time: 15+ minutes
A commercial diesel engine generates combustion temperature well above 1,500°F, while an aluminum cylinder head or engine block begins to soften and lose structural integrity around its 1,200°F melting point. This narrow thermal margin makes a proper coolant flush interval one of the most critical preventive maintenance decisions a fleet manager faces — unlike a passenger vehicle, a Class 6–8 truck operates under sustained load, an extended idle period, and a severe-duty cycle that accelerates coolant degradation far beyond a consumer-vehicle timeline.
The cooling system in a heavy-duty diesel represents far more than freeze protection. A modern extended-life coolant contains a specialized additive package engineered to prevent cavitation erosion on a wet-sleeve cylinder liner, inhibit scale formation in an EGR cooler, and protect the diverse metallurgy found in today's emissions-compliant powertrain. When these additives deplete, the consequence extends beyond overheating to include liner pitting, water pump failure, and EGR system damage that can sideline a truck for days.
Michael Nielsen and Heavy Duty Journal's editorial team built this guide around what genuinely determines coolant service timing — the Technology & Maintenance Council and an engine manufacturer provide specific guidance, but real-world fleet operation often demands more frequent attention based on duty-cycle severity. HDJ's diesel engine maintenance schedule guide covers where coolant service fits into the broader PM calendar.
Key Takeaways
- ✓OEM interval varies significantly: a heavy-duty diesel coolant service ranges from roughly 600,000 miles for a fully-formulated ELC to annual SCA testing for a conventional coolant.
- ✓Duty cycle determines the true interval: a severe-service operation including high idle time, a dusty environment, and frequent thermal cycling commonly needs a meaningfully shorter maintenance window than the published OEM figure.
- ✓Testing prevents guesswork: a regular coolant analysis using a test strip or a laboratory service identifies additive depletion before engine damage occurs.
- ✓Mixing coolant types creates failure: an incompatible formulation precipitates a protective additive out of solution, causing accelerated liner pitting and water pump seal degradation.
- ✓Proper procedure matters: a complete system flush removes a contaminant that a drain-and-fill method leaves behind in the block, EGR cooler, and heater core.
In This Guide
- Heavy-Duty Coolant Types and Their Service Requirements
- Factors That Accelerate Coolant Degradation in Fleet Operations
- Coolant Testing and Condition Monitoring
- The Professional Coolant Flush Process for Heavy-Duty Equipment
- Consequences of Neglected Coolant Maintenance
- Best Practices for Fleet Coolant Management
- Frequently Asked Questions
Heavy-Duty Coolant Types and Their Service Requirements
The commercial vehicle industry uses three primary coolant technologies, each engineered for a specific protection characteristic and maintenance interval. Understanding these formulations helps a fleet manager select the appropriate product and establish an effective PM schedule — the chemical difference between coolant types directly impacts how often the system needs service and what testing protocol applies.
Color coding provides general identification, but a fleet manager should verify coolant specification through OEM documentation rather than relying solely on visual cues. Several manufacturers use a similar color for a different formulation, and cross-contamination between incompatible products creates an expensive cooling system failure.
Conventional Coolants with Supplemental Coolant Additives
A traditional low-silicate antifreeze formulation remains common in an older heavy-duty application and certain regional preference. This conventional coolant relies on inorganic additive technology that depletes relatively quickly under the thermal stress of diesel operation — the protective compound requires regular replenishment through a Supplemental Coolant Additive (SCA) to maintain adequate liner protection.
A fleet using conventional coolant must test SCA concentration at every preventive maintenance interval — typically every 250 operating hours or roughly 15,000 miles, per major manufacturer specification. The ASTM D6210 specification defines the requirement for a fully-formulated heavy-duty engine coolant, including corrosion protection, cavitation resistance, and an SCA maintenance protocol. When a test strip indicates depleted additive, a technician adds SCA according to system capacity to restore protection. Complete coolant replacement occurs roughly every 2–3 years or 200,000–250,000 miles under normal service, with the exact figure varying by manufacturer.
The maintenance burden of a conventional coolant makes it increasingly rare in a modern fleet application, though some operations continue using it for lower initial cost or compatibility with legacy equipment. Proper SCA management prevents the cylinder liner cavitation erosion that occurs when additive level drops below a protective threshold.
Extended Life Coolants for Reduced Maintenance
Extended Life Coolant (ELC) formulations use organic acid technology providing significantly longer protection than a conventional product. A fully-formulated ELC from a major manufacturer typically specifies a service interval of up to 600,000 miles, 12,000 hours, or 6 years for an on-highway application, consistently confirmed across multiple manufacturer data sheets — a meaningfully longer interval that reduces maintenance cost and downtime while providing superior protection for modern diesel engine metallurgy.
The organic acid inhibitor in an ELC formulation works differently than a traditional additive. Rather than coating every metal surface, it forms a protective barrier specifically where corrosion initiates — a targeted approach that extends effective service life while reducing the deposit formation that can restrict coolant flow through an EGR cooler and charge air cooler passage.
Most heavy-duty engine manufacturers including Cummins, Detroit Diesel, PACCAR, and Navistar now factory-fill with an ELC formulation. This product requires less ongoing maintenance but demands strict attention to concentration level and contamination prevention — even a small amount of conventional coolant mixed into an ELC system can compromise the organic acid chemistry.
Hybrid Formulations and Nitrited Products
Hybrid Organic Acid Technology (HOAT) coolants combine an organic acid with a small amount of traditional additive to address a specific protection requirement. This product often includes a nitrite compound providing enhanced cavitation protection for a wet-sleeve diesel engine — the nitrite content requires periodic replenishment through an extender package, typically at a 300,000-mile interval.
A nitrite level in a heavy-duty cooling system requires monitoring, since this compound depletes faster than another protective additive. The Technology & Maintenance Council's RP 329 provides guidance on coolant maintenance for a fleet operation. A test strip or laboratory analysis can verify nitrite concentration remains within specification — a low nitrite level allows cavitation damage to a cylinder liner, creating pitting that eventually leads to coolant-to-oil contamination.
A fleet manager must verify compatibility when topping off or replenishing a HOAT system. A different manufacturer formulates its hybrid product with a varying additive ratio, and mixing an incompatible HOAT product can cause a precipitation that clogs a cooling system passage.
| Coolant Type | Service Interval | Testing Requirements | Primary Applications |
|---|---|---|---|
| Conventional + SCA | 2–3 years / 200,000–250,000 miles | Every PM interval | Legacy equipment, regional fleets |
| Extended Life (ELC) | 6 years / up to 600,000 miles / 12,000 hours | Annual or 150,000 miles | Modern on-highway Class 8 |
| Hybrid OAT (HOAT) | 5 years / 500,000–750,000 miles | Every 150,000 miles | Mixed-fleet operations |
| Nitrited ELC | 6 years / up to 600,000 miles + extender | Every 300,000 miles | Wet-sleeve diesel engines |
These figures reflect what's commonly published across major coolant manufacturers as of September 2026, but the exact number varies by brand and specific product — always confirm against the coolant manufacturer's own data sheet and the engine OEM's service manual for a specific fleet's equipment.
Free Diesel Maintenance Checklist
Get HDJ's free, field-tested diesel maintenance checklist delivered instantly to your inbox — print it, laminate it, keep it in the shop.
Instant PDF • 100% Free • No Spam
Factors That Accelerate Coolant Degradation in Fleet Operations
A published OEM interval assumes a normal operating condition that many commercial applications exceed regularly. A fleet manager must evaluate the specific duty cycle against the manufacturer's assumption to determine appropriate service timing — several operational factors accelerate coolant additive depletion and may call for a meaningfully shorter interval than the published specification.
Understanding these degradation factors lets a maintenance department implement a condition-based service interval rather than relying solely on mileage or calendar time. Proactive testing combined with duty-cycle awareness prevents the expensive cooling system failure that results from depleted coolant chemistry.
Extended Idle Operations and Thermal Cycling
A high-idle application places exceptional stress on a cooling system despite accumulating relatively few miles. A truck in a vocational application, a distribution route with a frequent stop, or any service requiring extended stationary operation experiences continuous thermal load without the airflow highway speed provides — the cooling system works harder per mile traveled, accelerating additive consumption.
Engine idle time should factor into maintenance scheduling for a fleet with significant stationary operation. Some fleet management systems track idle hours separately, letting a maintenance planner adjust coolant service based on total thermal exposure rather than mileage alone — an operation averaging more than 40% idle time may benefit from coolant testing at roughly twice the normal frequency.
Thermal cycling — repeated heating and cooling of the engine — also stresses coolant chemistry. A distribution truck making numerous daily stops experiences more thermal cycles than a long-haul operation covering equivalent mileage, and each cycle subjects the additive package to chemical stress that accumulates over time.
Environmental and Operating Conditions
Climate extreme affects coolant service requirement in both directions. An operation in a consistently hot climate above 95°F experiences accelerated additive depletion as the cooling system operates near maximum capacity continuously — the sustained thermal load breaks down a protective compound faster than a moderate-climate operation, and a hot-climate fleet may benefit from a meaningfully shortened testing interval.
A cold-climate operation presents a different challenge. A frequent cold start before achieving full operating temperature creates condensation within the cooling system, and this moisture dilutes coolant concentration and introduces a corrosive element. Road salt exposure and increased stop-and-go driving in winter weather also contribute to accelerated degradation.
A dusty environment introduces an airborne contaminant that eventually reaches the cooling system through make-up water or a contaminated service procedure. Construction, mining, and agricultural applications often need more frequent coolant maintenance due to environmental exposure — these severe-service operations benefit from laboratory coolant analysis rather than relying on a field test strip alone.
Equipment Age and System Condition
A high-mileage piece of equipment with accumulated cooling system deposit needs more vigilant maintenance than a newer truck. An internal scale and corrosion product from years of operation creates a rough surface where additional corrosion initiates more readily — even a fresh coolant degrades faster in an aged system, since the additive must work harder to protect a compromised surface.
Previous maintenance history significantly impacts current requirement. Equipment with an inconsistent coolant service record, an unknown service history from prior ownership, or evidence of coolant contamination may need immediate flushing regardless of apparent condition — starting fresh with a documented coolant chemistry establishes a reliable baseline for future maintenance planning.
A cooling system component also influences service timing. An aging rubber hose sheds a particle into coolant circulation, and a deteriorating gasket material introduces a contaminant. Equipment approaching a major cooling system component replacement may benefit from accelerated coolant service to evaluate system condition comprehensively.
Coolant Testing and Condition Monitoring
Effective coolant maintenance depends on accurate condition assessment rather than an arbitrary time or mileage interval. Testing provides objective data on additive concentration, contamination level, and remaining service life — a fleet operation should establish a testing protocol that identifies a problem before it causes equipment damage or an unscheduled downtime.
Multiple testing options exist at a different cost and accuracy level. A field test strip provides an immediate result during a routine PM service, while laboratory analysis delivers a comprehensive chemistry profile for a detailed condition assessment — most fleets benefit from combining both approaches based on equipment criticality and operating condition.
Field Testing with Coolant Test Strips
A test strip provides a rapid indication of a key coolant parameter during a preventive maintenance inspection. A quality test strip measures freeze point protection, pH level, and SCA or nitrite concentration depending on strip configuration, with a result appearing within 30–60 seconds, letting a technician make an immediate service decision.
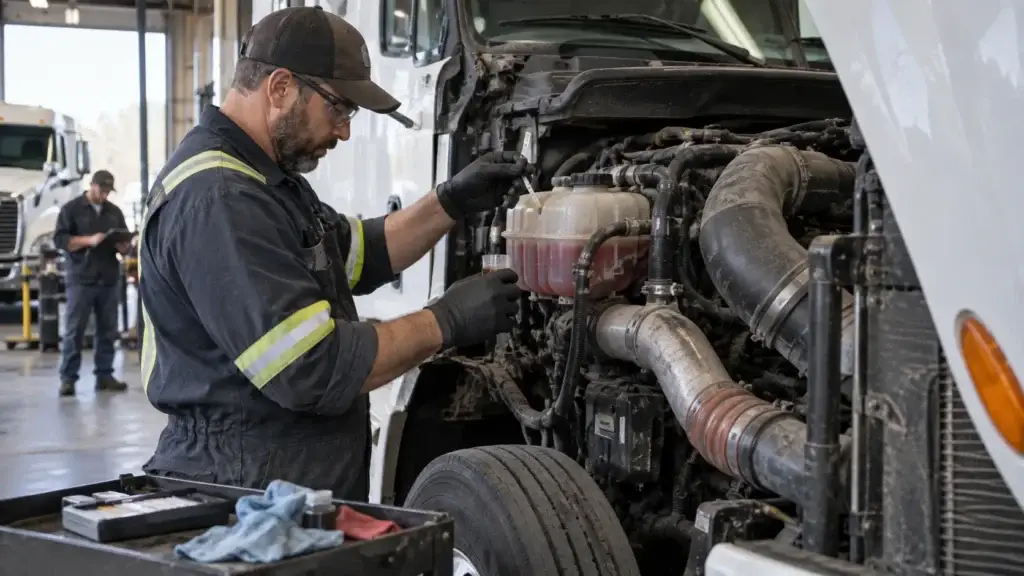
Proper technique ensures an accurate result. Collect a sample from the mid-system using the radiator petcock or a sampling port rather than the overflow reservoir. Allow the engine to reach operating temperature before sampling to ensure circulation has mixed the coolant thoroughly, and follow the manufacturer's timing precisely when reading a color-change indicator.
A test strip has a real limitation, including an inability to detect certain contaminants and reduced accuracy compared to a laboratory method. This tool works well for routine monitoring but should be supplemented with periodic laboratory analysis for a comprehensive condition assessment — any anomalous test strip result warrants confirmation through laboratory testing before a major service decision.
Laboratory Coolant Analysis
Professional laboratory analysis provides a detailed coolant chemistry profile identifying a developing problem field testing can't detect. This service measures a specific additive concentration, identifies a contamination source, and detects a condition like glycol degradation or silicate gel formation — a major oil analysis provider offers a coolant testing program structured for a fleet account.
A laboratory sample requires proper collection and handling to ensure an accurate result. Use a clean sample container provided by the testing laboratory and collect a sample at normal operating temperature. Complete the sample information form accurately, including coolant type, equipment identification, and operating hours or mileage, then ship the sample promptly to prevent degradation during transit.
Trending a laboratory result over time reveals a gradual change an individual sample might not indicate. Establish a baseline value for each equipment unit and monitor for deviation from the normal pattern — a sudden change in any parameter warrants investigation even if the value remains within an acceptable range.
Visual Inspection and Warning Signs
Physical inspection provides valuable condition information between a formal testing interval. Check coolant level and appearance weekly or at every fuel stop for a critical piece of equipment — several visual indicators signal a cooling system problem requiring immediate attention rather than waiting for scheduled testing.
Discoloration from the original coolant color indicates contamination or degradation. A rust-brown coloring suggests internal corrosion, while a milky appearance indicates oil contamination from a failed gasket or a cooler leak. Any floating particle, sludge accumulation, or unusual odor warrants immediate investigation and likely system service.
Temperature gauge behavior provides an early warning of a cooling system problem. A fluctuating reading, a higher-than-normal operating temperature, or an extended warm-up time may indicate restricted flow from a degraded coolant or a failing component — address a temperature anomaly promptly before it progresses to equipment damage.
The Professional Coolant Flush Process for Heavy-Duty Equipment
A complete coolant flush removes an accumulated contaminant, a degraded additive, and a corrosion product that a simple drain-and-refill procedure leaves behind. Professional flushing reaches every cooling system passage including the engine block, EGR cooler, heater core, and radiator tube — the process ensures the new coolant provides maximum protection without dilution from a residual contaminated fluid.
A heavy-duty cooling system holds roughly 10–15 gallons depending on configuration, and proper flushing requires equipment capable of handling this volume efficiently. The investment in a thorough service prevents the cascading failure that results from contamination carry-over between a coolant change.
Pre-Flush Inspection and Preparation
A thorough inspection before flushing identifies a component failure requiring attention during the service. Check every hose for a crack, a soft spot, or a bulge indicating imminent failure. Examine belt condition and tension, the water pump weep hole for seepage, and every connection for evidence of a leak.
Document the existing coolant type and any known contamination history. This information determines the appropriate flush procedure and identifies whether multiple flush cycles may be necessary to remove an incompatible residue — a severely contaminated system, or one transitioning between coolant types, often needs an extended flushing protocol.
Verify the replacement coolant matches OEM specification for the equipment being serviced. Have sufficient quantity on hand to complete the service, including a reserve needed for topping off after initial air bleeding. Pre-mixing coolant concentrate with distilled water ensures a proper protection level from the first fill.
Flush Execution and System Cleaning
Begin by draining existing coolant from every accessible drain point. A heavy-duty application typically has multiple block drains plus a radiator and heater core drain — opening every drain simultaneously removes the maximum fluid volume. Capture and properly dispose of every used coolant according to EPA antifreeze recycling guideline, which prohibits dumping a waste antifreeze into a storm drain, septic system, or surface water.
Professional flush equipment uses pressurized flow to dislodge a contaminant throughout the system, reversing flow direction multiple times to push a loosened deposit out of the passage where it accumulated. A chemical cleaner formulated for a heavy-duty cooling system dissolves scale and residue without damaging a gasket or seal.
Continue flushing until discharge runs completely clear with no visible contamination. A system with heavy scale or silicate gel may need an extended flush time or multiple cleaning cycles — never shortcut this process, since a contaminant remaining after flushing will compromise the new coolant chemistry immediately.
Refilling and Air Removal
Refill the system with pre-mixed coolant, or a carefully measured concentrate and distilled water, to achieve a proper protection level. A heavy-duty system requires attention to fill procedure because its complex routing creates multiple air trap points — many modern trucks include a dedicated bleed port or an automatic air purge system.
An air pocket trapped in the cooling system causes a localized overheating and reduces overall cooling efficiency. Run the engine with the pressure cap removed, cycling the heater control to full hot. Monitor the radiator neck for an air bubble release and add coolant as the level drops from air displacement.
Verify proper fill by running the engine through a complete warm-up cycle and rechecking the level after cooldown. Some systems need multiple heat cycles to fully purge air from the passages. Document the coolant type and date of service for future maintenance reference.
Consequences of Neglected Coolant Maintenance
The financial impact of inadequate coolant maintenance extends far beyond the cost of a replacement fluid. A cooling system failure causes an unscheduled downtime, an emergency roadside repair, and a cascading damage to an expensive engine component. Understanding these consequences helps justify appropriate investment in a preventive maintenance program.
A heavy-duty diesel engine represents an investment of $20,000–$50,000 or more, and a cooling-related failure can total this powerplant. The modest expense of proper coolant maintenance provides an exceptional return on investment compared to a major repair cost.
Cylinder Liner Cavitation and Pitting
A wet-sleeve diesel engine faces particular vulnerability to cavitation erosion when coolant protection fails. The combustion pressure pulse creates a cylinder liner vibration that generates a vapor bubble in adjacent coolant — when this bubble collapses against the liner surface, it creates a microscopic impact that erodes metal over time.
An adequate nitrite or other cavitation inhibitor concentration prevents this erosion by modifying bubble formation characteristics. When additive level drops below a protective threshold, pitting accelerates sharply — advanced pitting eventually penetrates the liner wall, allowing coolant to enter the cylinder and oil to contaminate the cooling system.
Liner replacement requires major engine disassembly, with associated labor cost typically running $5,000–$10,000 depending on the engine platform, as of September 2026. Catching a depleted additive level through regular testing prevents this expensive failure mode.
EGR Cooler and Aftertreatment Damage
A modern emissions-compliant diesel routes exhaust gas through a cooler that depends on effective coolant circulation. A scale deposit from a degraded coolant restricts flow through this heat exchanger, reducing cooling efficiency and increasing exhaust gas temperature. A failed EGR cooler can leak coolant into the intake system, causing hydro-lock and catastrophic engine damage.
An aftertreatment system downstream of the engine also suffers from cooling system neglect. A DEF injection system and DPF regeneration depend on proper engine temperature management — a cooling problem causing elevated temperature can damage an SCR catalyst and create a DPF issue that triggers an expensive derate or a forced regeneration cycle. HDJ's diesel emission control guide covers how EGR cooler damage cascades into the rest of the aftertreatment system.
An EGR cooler replacement cost typically runs $1,500–$4,000 plus associated labor and downtime. Preventive coolant maintenance protects these emissions components along with the core engine system.
Water Pump and Radiator Failures
A contaminated or acidic coolant attacks a water pump seal and bearing, causing premature failure. A particle from a corroding system component acts as an abrasive that accelerates wear on a pump impeller and sealing surface — water pump replacement typically costs $500–$1,500 for most heavy-duty applications, plus the downtime impact of unscheduled service.
A radiator tube becomes restricted by a scale deposit and a corrosion product circulating in a neglected cooling system. This restriction reduces heat rejection capacity, causing an elevated operating temperature even before complete blockage occurs — a heavy-duty radiator replacement typically runs $1,000–$3,000 depending on cooling package configuration.
These component failures often occur roadside rather than in the shop, multiplying cost through an emergency service fee, towing, and an extended downtime awaiting a part. Preventive coolant maintenance keeps a truck running reliably and scheduled for in-shop service at a convenient time.
Best Practices for Fleet Coolant Management
Effective coolant management combines appropriate product selection, consistent service procedure, and accurate record-keeping. A fleet operation benefits from standardizing coolant type where possible and establishing a clear protocol every technician follows — these practices maximize equipment protection while controlling maintenance cost.
Documentation proves particularly important for cooling system maintenance. A service record should include coolant type, quantity added, test result, and any anomaly observed. This history informs a future maintenance decision and supports a warranty claim when a component failure occurs.
Standardization and Product Selection
Select a coolant product that meets or exceeds OEM specification for the fleet's equipment mix. Where multiple equipment brands operate in the same fleet, identify a coolant formulation compatible with every platform to enable standardization — maintaining a single coolant type simplifies inventory, prevents a cross-contamination error, and ensures a technician always uses the correct product.
Purchase coolant from a reputable supplier who can provide a product specification and technical support. A bulk purchase reduces the per-gallon cost for a larger fleet but requires proper storage to prevent contamination or degradation — store coolant in a sealed container away from direct sunlight and a temperature extreme.
Avoid a "universal" coolant claiming compatibility with every formulation. This product may not provide optimal protection for a specific piece of equipment and can complicate troubleshooting when a problem develops — match coolant chemistry to the engine requirement rather than seeking a one-size-fits-all solution.
Service Procedures and Training
Establish a written procedure for coolant testing, topping off, and a complete flush service. This procedure should specify a proper collection technique, an acceptable parameter range, and an escalation protocol when a test result indicates a problem — a consistent procedure ensures a reliable result regardless of which technician performs the service.
Train a technician on cooling system fundamentals including additive chemistry, a contamination source, and a proper testing method. Understanding why a procedure matters improves compliance and helps a technician identify a developing problem during a routine inspection — many coolant manufacturers offer a training resource for fleet maintenance personnel.
Invest in quality testing equipment and verify its accuracy periodically. An expired or improperly stored test strip provides an unreliable result that may miss a critical problem or trigger an unnecessary service. Replace testing supplies according to the manufacturer's schedule and store them properly between uses.
Frequently Asked Questions
How often should heavy-duty diesel trucks receive coolant flush service?
It depends on coolant type and operating condition. An Extended Life Coolant typically calls for complete replacement at up to 600,000 miles, 12,000 hours, or 6 years under normal service. A conventional coolant with SCA needs replacement roughly every 2–3 years or 200,000–250,000 miles. Severe duty — high idle time, extreme temperature, dust — may need a meaningfully shorter interval. Regular testing gives the most accurate read.
Can different coolant types be mixed in an emergency?
Mixing an incompatible formulation creates a chemical reaction that precipitates a protective additive out of solution, neutralizing protection for both products. If an emergency top-off requires a different type, flush and refill with the correct product as soon as possible — a small contamination volume may allow continued operation until scheduled service, but significant mixing needs immediate attention.
What causes cylinder liner pitting in diesel engines?
Cavitation erosion when coolant additive level drops below a protective threshold. The combustion pressure pulse creates liner vibration that generates a vapor bubble in adjacent coolant; when the bubble collapses against the liner surface, the impact erodes metal progressively. Adequate nitrite or SCA concentration prevents this — regular testing and replenishment protects a liner throughout its service life.
How do I determine if my fleet needs more frequent coolant testing?
Several factors indicate a shorter interval: extended idle exceeding 40% of engine runtime, extreme climate exposure, a dusty or contaminated environment, equipment with an unknown maintenance history, and any truck showing a temperature gauge anomaly or visible deterioration. A fleet with these conditions benefits from testing at roughly twice the normal interval.
What is the proper coolant concentration for heavy-duty applications?
The standard recommendation is a 50/50 concentrate-to-water ratio, providing freeze protection to roughly -34°F and boilover protection to roughly 265°F under pressure. Some severe cold-climate operations use a 60/40 ratio for additional freeze protection, though a higher concentrate percentage reduces heat transfer efficiency. Always use distilled water — tap water mineral causes scale that restricts flow.
Should I use laboratory analysis or field test strips for coolant monitoring?
Most fleets benefit from combining both. A field test strip provides a rapid result during routine PM, enabling an immediate decision on additive replenishment or gross contamination. Laboratory analysis delivers a comprehensive profile identifying a subtle problem a strip can't detect. Use field testing at every PM interval and supplement with laboratory analysis annually or when a result needs confirmation.
Conclusion
A coolant flush interval directly impacts fleet reliability, maintenance cost, and equipment longevity. A heavy-duty diesel operates under sustained thermal load that demands proper cooling system protection, and modern emissions equipment adds a component vulnerable to coolant-related damage. Understanding a specific coolant type's requirement and adjusting the service interval for actual duty-cycle severity protects the equipment investment effectively.
The modest expense of proper coolant maintenance — testing, additive, and periodic flushing — returns substantial value through prevented failure. Cylinder liner replacement, EGR cooler damage, and a roadside breakdown each cost thousands of dollars, making preventive service clearly cost-effective. Establish a testing protocol appropriate for the operation, document every coolant service, and respond promptly when a result indicates a developing problem — the same discipline Michael Nielsen and Heavy Duty Journal's editorial team hold every guide on heavydutyjournal.com to.
Review the fleet's current coolant maintenance practice against the guideline in this article. Verify that the service interval matches both OEM specification and actual operating condition. Implement regular testing if not already standard practice, and ensure a technician understands the proper procedure for sampling, interpretation, and a service decision — these steps protect a cooling system from the expensive failure that results from neglected maintenance.
Help Fellow Fleet Professionals
This coolant maintenance guide can help other fleet managers and technicians prevent an expensive cooling system failure — share it with a colleague who maintains heavy-duty equipment.