By Michael Nielsen, Publisher | 15+ Years in Diesel Repair
Last Updated: September 2026
⏱ Estimated reading time: 15+ minutes
Truck corrosion prevention for fleets means combining regular washing, protective undercoating, and scheduled inspections to stop road salt and moisture from attacking a vehicle's frame, body, and electrical systems before they cause structural damage or a roadside failure. An effective program starts with identifying a high-risk corrosion zone — a frame rail, cross member, wheel well, and electrical connector — then applying the right coating for each area and inspecting on a fixed interval rather than waiting for visible rust to appear.
Michael Nielsen and Heavy Duty Journal's editorial team built this guide because corrosion isn't a cosmetic problem for a fleet manager or diesel technician. A rusted frame rail can trigger a roadside out-of-service order under North American Standard inspection criteria, and a corroded wiring harness causes the kind of intermittent electrical fault that eats up diagnostic hours in the shop.
This guide covers how corrosion forms, which components fail first, how undercoating products compare, and how to structure a preventive maintenance (PM) program that holds up through a full winter of road salt exposure.
Key Takeaways
- ✓Chloride-based de-icers are the real driver: a sodium, magnesium, and calcium chloride brine conducts electrical current across a truck's frame and body, turning ordinary surface moisture into an active corrosion cell — plain water alone rarely causes this level of damage.
- ✓A cracked or badly corroded frame can take a truck out of service on the spot: under CVSA's North American Standard Out-of-Service Criteria, a frame corrosion that compromises structural integrity is a roadside violation, and the vehicle may have to be towed rather than driven to a shop.
- ✓Coating choice depends on the vehicle's rust stage, not personal preference: a lanolin-based product is the better call once surface rust has already started because it displaces trapped moisture; a hard rubberized coating should only go on clean, rust-free steel because it can trap water against bare metal if applied over existing corrosion.
- ✓Electrical grounds fail quietly and expensively: a corroded battery terminal and chassis ground point causes a voltage drop and false fault code long before anyone notices visible rust, making it one of the highest-value places to focus a corrosion prevention budget.
In This Guide
- How Road Salt and De-Icing Chemicals Accelerate Truck Corrosion
- High-Risk Corrosion Zones on Commercial Trucks and Trailers
- Truck Frame Corrosion and CVSA Out-of-Service Risk
- Undercoating and Rustproofing Options for Fleet Vehicles
- Building a Fleet Corrosion Prevention Program
- Electrical and Component-Level Corrosion Protection
- Weighing the Cost of Corrosion Prevention Against Repair and Downtime
- Frequently Asked Questions
How Road Salt and De-Icing Chemicals Accelerate Truck Corrosion
Road salt accelerates truck corrosion by dissolving into an electrolyte solution on contact with moisture, which conducts electrical current across a vehicle's metal surfaces and dramatically speeds up the natural oxidation process. Corrosion itself is an electrochemical reaction: iron in steel loses electrons to oxygen in the presence of water, forming iron oxide — the reddish-brown flaking most people simply call rust.
Plain rainwater causes this reaction slowly. A chloride-based de-icer changes the chemistry entirely, because a de-icing salt supplies an unusually efficient electrolyte for that process. Sodium chloride is the most common winter de-icer, but many states and provinces have shifted toward a magnesium chloride and calcium chloride brine because it works at a lower temperature.
Both are hygroscopic — they pull moisture out of the air — which means a treated pavement stays wet longer after a storm than it would with rock salt alone, extending the window during which a truck's undercarriage sits in a corrosive film.
A galvanic corrosion adds a second failure mode fleets often overlook. It occurs when two dissimilar metals — say, an aluminum wheel and a steel hub, or a stainless fastener threaded into a mild-steel bracket — are in contact in the presence of an electrolyte, causing the more reactive metal to corrode faster than it would on its own.
A salt brine is an excellent electrolyte, so any fleet running a mixed-metal component (aluminum wheels, steel frames, brass fittings) sees an accelerated failure at those junction points specifically, not uniformly across the vehicle.
Most state departments of transportation continue expanding a brine pre-treatment program because it reduces salt volume and cost per lane-mile, which means the corrosive chemistry fleets deal with each winter is shifting toward a chloride mix rather than away from it. That trend makes chemical exposure — not just visible snow and ice — the metric worth tracking when planning a corrosion prevention budget.
Do Electronic Corrosion Protection Systems Actually Work?
An electronic corrosion protection system, sometimes called an impressed-current or cathodic protection system, works by running a small electrical current through the truck's metal structure to interrupt the electrochemical reaction that produces rust. A handful of fleets have adopted these systems as a supplement to — not a replacement for — coating and washing. Results reported by users are mixed, and the physics behind cathodic protection is well established in marine and pipeline applications at a much larger scale than a single truck frame.
For most fleets, an electronic system is worth considering only after the fundamentals — washing, undercoating, and inspection — are already locked into the PM schedule, not as a shortcut around them.
High-Risk Corrosion Zones on Commercial Trucks and Trailers
The highest-risk corrosion zones on a commercial truck are the areas where moisture collects and airflow is limited — a frame rail and cross member, a wheel well, a battery box, and any cavity where road spray settles and never fully dries. Corrosion rarely starts on a broad, exposed surface; it starts in the seam, pocket, and boxed section that stays damp long after the rest of the vehicle has dried out.
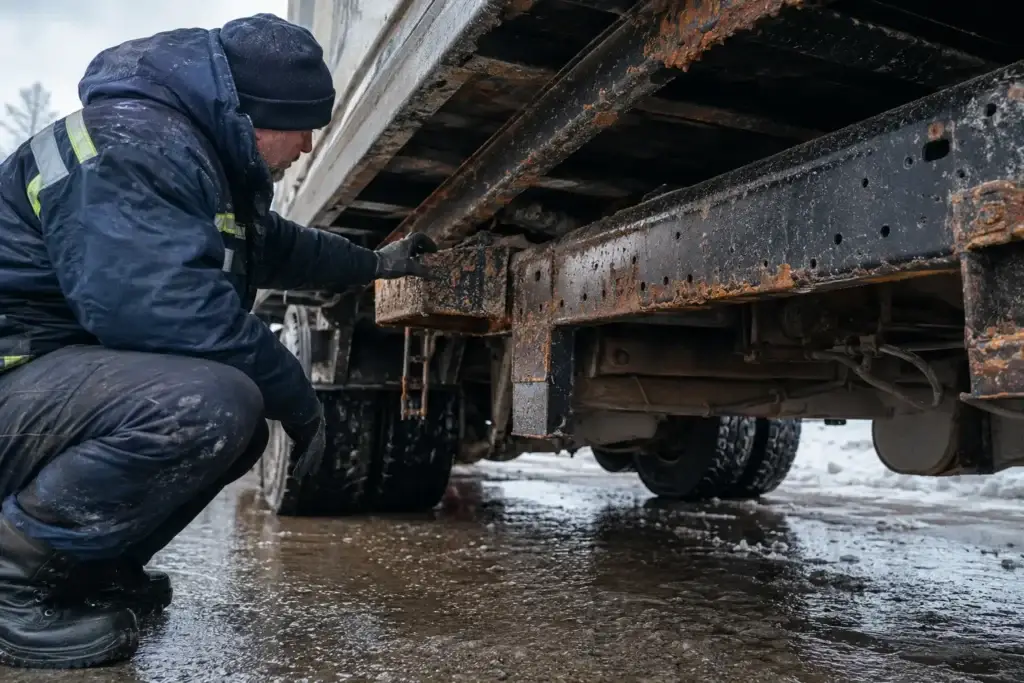
A frame rail and cross member takes the most direct hit from road spray and is also the most structurally consequential — sustained exposure at these points can undermine both the rail's structural integrity and the vehicle's load capacity over time.
A brake and fuel line runs a close second: a steel and aluminum-alloy line is prone to a pitting corrosion that eats through the wall from the outside in, which turns a slow-forming cosmetic issue into a direct safety liability once the line wall thins enough to leak or fail under pressure.
HDJ's air brake troubleshooting guide covers how the same road salt exposure specifically attacks an air tank and its mounting bracket.
A wheel-end hardware deserves its own line item on any inspection sheet, because a corrosion that reaches the wheel end through a displaced grease seal can trigger a premature failure of a component that's directly safety-critical. A battery terminal and chassis ground point round out the highest-priority zones.
These corrode quietly — without the visible flaking that shows up on frame steel — and the result is often a voltage drop, a false sensor reading, or an intermittent fault that gets misdiagnosed as an electronic control module (ECM) problem when the real cause is a green crust on a ground strap.
| Corrosion Zone | Why It's Vulnerable | Recommended Inspection Interval |
|---|---|---|
| Frame rails & cross members | Direct road spray exposure; boxed sections trap brine | Every PM service; detailed check quarterly |
| Wheel ends & hub assemblies | Grease seal displacement lets moisture reach bearings | Every PM service |
| Brake & fuel lines | Pitting corrosion weakens line walls from the outside in | Every PM service |
| Battery terminals & chassis grounds | Silent voltage drops; often misdiagnosed as ECM faults | Monthly, or at every driver pre-trip |
| Wiring harness connectors | Backshell seals degrade, letting brine wick into pins | Quarterly |
Truck Frame Corrosion and CVSA Out-of-Service Risk
Frame corrosion becomes a regulatory problem, not just a maintenance one, the moment it compromises the structural integrity of the rail — at that point it can trigger an out-of-service order during a roadside inspection. The Commercial Vehicle Safety Alliance (CVSA) publishes the North American Standard Out-of-Service Criteria (OOSC), the pass-fail standard inspectors use to decide whether a driver, vehicle, or cargo presents an imminent hazard.
Federal regulation backs this up directly. 49 CFR 393.201 states that the frame or chassis of a commercial motor vehicle shall not be cracked, loose, sagging, or broken, and that any welded repair of the frame must follow the vehicle manufacturer's recommendations — a detail that matters because a corrosion-thinned steel often fails a weld repair that would hold fine on undamaged rail.
Separately, 49 CFR 396.3 requires every motor carrier to systematically inspect, repair, and maintain every vehicle under its control, with a part and accessory kept in safe and proper operating condition at all times — a corroded frame component falls squarely inside that requirement.
⚠️ Safety Warning
A frame rail with corrosion severe enough to compromise structural support is an out-of-service condition, and the vehicle typically cannot be driven to a repair facility — it must be towed. Never attempt a field weld repair on a corroded frame section without first confirming manufacturer-approved procedures under 49 CFR 393.201(d); welding over thinned or pitted steel can create a repair that fails faster than the corrosion it was meant to fix.
Inspectors specifically call out corrosion on a frame and structural checklist — not as a minor cosmetic note, but as a defect category on par with a cracked or bent rail. Building a corrosion inspection step into every pre-trip and PM interval, rather than waiting for the annual inspection required under Part 396, is the difference between catching a pitting while it's still surface-level and discovering a rail that's already lost enough wall thickness to fail under normal load.
Undercoating and Rustproofing Options for Fleet Vehicles
Undercoating is a sprayed-on protective barrier applied to a vehicle's undercarriage — a frame rail, floor pan, wheel well, and control arm — to block moisture and a de-icing chemical from reaching bare steel. Rustproofing is the broader term, typically covering the undercarriage plus an internal cavity like a door panel, rocker panel, and tailgate seam, often through a small drilled access hole that gets plugged after treatment.
Three coating families dominate the fleet market, and choosing wrong can do more harm than doing nothing. A lanolin-based coating, sold under names like Fluid Film and Woolwax, stays soft and pliable indefinitely and never forms a hard shell, which lets it creep into a seam through capillary action and displace moisture that's already trapped against the metal.
A wax-based product is cheaper and works well on a clean, rust-free vehicle but offers moderate protection and typically needs reapplication within a year. A rubberized and asphalt-based coating provides the best resistance to rock and gravel impact on an exposed frame area, but it forms a hard shell — one that can crack, and once cracked, seal moisture against the frame rather than keeping it out.
That last point is the one that trips up a fleet buying on price alone: never apply a hard rubberized or asphalt coating over existing surface rust. Once a frame already shows oxidation, a lanolin-based product is almost always the safer call, since it works with the moisture already present rather than trying to seal against it.
| Coating Type | Typical Reapplication | Best Suited For | Avoid If |
|---|---|---|---|
| Lanolin-based (Fluid Film, Woolwax) | 1–2 years | Vehicles with existing surface rust; seams and cavities | You need maximum impact/abrasion resistance |
| Wax or paraffin-based | Several months to 1 year | New or rust-free vehicles; budget-conscious PM cycles | Frame already shows pitting or scale |
| Rubberized / asphalt-based | 3–5 years (until cracking) | High rock/gravel impact zones on clean steel | Any existing rust is present beneath the coating |
A product formulation standard matters here too. A coating durability claim is commonly tested using an accelerated corrosion method such as the ASTM B117 salt spray (fog) test, which exposes a coated and uncoated metal sample to a controlled saline mist to generate comparative corrosion-resistance data. It's worth asking any undercoating vendor whether their published protection claims are backed by B117 or equivalent testing rather than marketing language alone.
Application Best Practices for Fleet Undercoating
Undercoating only performs as well as the surface prep behind it. The frame needs to be washed and fully dry before application — coating over trapped moisture or road grime seals the problem in rather than keeping it out. A fleet running its own application program typically uses a pressure gun with an extension wand to reach a boxed frame section and door cavity, while a lanolin product's low viscosity when warm makes it easier to push through a small access hole than a thicker rubberized compound.
Whether the work is done in-house or through a mobile service, the same rule applies: apply before the first hard freeze of the season, not during it, since a cold product atomizes poorly and coats unevenly compared to a thin, even film applied at moderate temperatures.
Building a Fleet Corrosion Prevention Program
A fleet corrosion prevention program combines four fixed elements — regular washing, seasonal undercoating, scheduled inspection, and driver reporting — applied on a calendar rather than left to individual judgment. HDJ's preventive maintenance checklist guide covers where a corrosion check fits into the broader annual and seasonal PM schedule. A fleet that treats corrosion prevention as an ad hoc task rather than a scheduled PM line item tends to see it slip during the exact months — deep winter — when it matters most.
Washing comes first because it's the cheapest and most effective step available, but soap choice matters more than a fleet tends to assume — an all-purpose detergent formulated for general road film won't fully break down the chloride residue left by a modern brine-based de-icer, particularly magnesium chloride. A specialized detergent designed specifically for de-icing chemical removal earns its higher cost in winter months for exactly that reason.
Washing frequency should scale with exposure: a fleet running a lane treated with liquid chloride brine needs more frequent washing than a fleet in a region using dry rock salt alone, because a brine residue clings to a painted and unpainted surface longer.
Undercoating should be scheduled before winter exposure begins, not after damage is already visible. A trailer and fleet vehicle is built predominantly from iron and steel, which are among the most corrosion-prone structural metals in common use — a fact that makes timing the coating application matter almost as much as the product choice itself. A pre-winter coating application, timed to a fresh wash and dry cycle, does more good than the same product applied mid-February onto a frame that's already carrying three months of accumulated brine.
Inspection is the third leg, and it needs to be a documented step on the PM checklist, not a verbal reminder to "keep an eye on it." Pair the inspection interval from the High-Risk Corrosion Zones table above with driver-reported defects: a driver who notices a new patch of surface rust during a pre-trip walk-around and reports it through the standard vehicle inspection report gives the shop weeks of lead time that a scheduled quarterly inspection alone would miss.
Documenting the Program for DOT and CVSA Review
A corrosion prevention program does double duty as compliance documentation. A maintenance record showing scheduled undercoating, wash frequency, and corrosion-specific inspection findings gives a fleet a paper trail if a frame defect is ever disputed during a roadside stop or a DataQ challenge, and it satisfies part of the systematic inspection, repair, and maintenance recordkeeping that 49 CFR 396.3 already requires every motor carrier to keep.
A fleet that logs a corrosion finding as a distinct category — rather than burying it inside a general "frame inspection" note — can also spot which trucks, routes, or yards are seeing a disproportionate corrosion and adjust a coating schedule or washing contract accordingly.

Electrical and Component-Level Corrosion Protection
Electrical and component-level corrosion protection focuses on the connector, terminal, and ground where even a small amount of oxidation causes an outsized diagnostic problem — a dielectric grease, terminal protectant spray, and sealed connector backshell are the primary tools. Unlike frame corrosion, which announces itself visually, an electrical corrosion hides inside a connector shell and shows up only as an intermittent fault code, a slow crank, or a sensor reading that drifts without explanation.
A battery terminal is the highest-frequency failure point. A thin coat of dielectric grease or a felt anti-corrosion washer at the terminal stops the white or blue crusty buildup that forms when battery acid vapor meets a road salt residue.
A chassis ground strap deserves the same attention — a ground point corroded down to a thin conductive path can still pass a basic continuity check while causing a voltage drop that manifests as dim lighting, slow starter engagement, or an electronic control module (ECM) communication error that sends a technician chasing the wrong module.
HDJ's brake chamber replacement guide covers a related pattern — rust perforation and cage bolt corrosion driven by the same road salt exposure, just on a brake component instead of an electrical one.
A wiring harness connector, particularly one routed near the frame rail or wheel well, relies on a rubber backshell seal that hardens and cracks with age and temperature cycling. Once that seal fails, capillary action pulls brine directly into the pin cavity — the same physics that makes a lanolin-based undercoating effective works against a fleet here, wicking corrosive moisture deep into a connector where it can't be seen or wiped away.
Replacing a cracked backshell seal during a PM visit costs a few dollars in parts; replacing the harness after an internal pin corrosion sets in can run into hundreds of dollars in parts and diagnostic labor.
DEF System and Sensor Corrosion
Diesel exhaust fluid (DEF) is itself a corrosive agent to the wrong material, which makes a DEF tank sending unit, dosing module connector, and NOx sensor harness another component-level corrosion zone worth its own attention.
DEF is engineered to be compatible with stainless steel, certain plastics, and specific alloys, but any connector or fitting that isn't rated for DEF contact — including a corroded ground or a cracked seal that lets road-salt moisture mix with a minor DEF leak at a fitting — can develop a crystallized deposit that interferes with electrical contact or restricts fluid flow.
A technician who sees a DEF-related fault code should check the connector and ground condition around the dosing module before assuming the sensor itself has failed.
Weighing the Cost of Corrosion Prevention Against Repair and Downtime
Corrosion prevention costs a fraction of what a corrosion-related repair and downtime cost, which makes it one of the easiest maintenance line items to justify to ownership even on a lean budget. A professional undercoating application and a specialized de-icing detergent both add a modest, predictable cost to a routine PM cycle — trivial next to the cost of an unplanned frame repair, a towed roadside breakdown, or the diagnostic labor spent chasing an intermittent fault back to a corroded ground strap.
Repair and maintenance spending is already one of the categories fleets are watching most closely. Per ATRI's 2026 Analysis of the Operational Costs of Trucking, the industry-average cost to operate a truck reached $2.336 per mile in 2025 — the highest per-mile cost in the report's history — with repair and maintenance rising 8.6% year over year, among the fastest-growing line items in the report.
Corrosion-related work doesn't show up as its own line in that data, but every avoidable frame repair, tow bill, or diagnostic comeback lands inside a cost category fleets are already under pressure to control.
The math holds up even for an owner-operator running a single truck. Prevention spending is scheduled, predictable, and shows up on a maintenance calendar; corrosion repair spending is unscheduled, disruptive, and almost always shows up at the worst possible time — mid-route, during a roadside inspection, or right before a load is due.
Resale and trade-in value add another layer to the calculation that fleets often leave out. A visibly corroded frame or a truck with rust bleeding through a wheel well and cab mount signals deferred maintenance to any buyer or appraiser, regardless of how well the drivetrain has been cared for, and it invites a harder negotiation on trade-in value than a clean undercarriage would.
A fleet that documents a consistent corrosion prevention program — the same record kept for DOT compliance — can point to that history when negotiating a sale or trade, turning a maintenance cost into evidence of asset care.
Frequently Asked Questions
How often should a fleet undercoat trucks for rust prevention?
Most a fleet operating in a road-salt region should apply a lanolin-based undercoating once a year, typically in early fall before winter chloride exposure begins. A wax-based product may need reapplication twice a year depending on wash frequency and mileage, while a rubberized coating can last three to five years but should be inspected annually for cracking.
Can a truck fail inspection because of rust?
Yes. Under CVSA's North American Standard Out-of-Service Criteria and 49 CFR 393.201, a frame or chassis that's cracked, sagging, or structurally compromised by corrosion is a critical violation that can place the vehicle out of service on the spot, regardless of how it looks from the driver's seat.
Is lanolin or wax-based undercoating better for trucks with existing rust?
A lanolin-based coating is the better choice for a truck that already shows surface rust, because it stays soft, penetrates seams through capillary action, and displaces trapped moisture rather than sealing over it. A hard wax, rubberized, or asphalt-based coating should generally be reserved for clean, rust-free steel.
What causes electrical corrosion on truck battery terminals?
Electrical corrosion at a battery terminal typically forms when acid vapor from the battery combines with a road salt residue and moisture, producing a white, green, or blue crusty deposit that increases resistance and causes a voltage drop. Dielectric grease and a felt anti-corrosion washer are standard preventive measures.
Does magnesium chloride cause more corrosion than regular road salt?
Magnesium chloride and calcium chloride brines are hygroscopic, meaning they pull moisture from the air and keep a treated surface wet longer than dry rock salt (sodium chloride) alone. That extended wet exposure — rather than the chemical itself being dramatically more corrosive per application — is the main reason a fleet in a state using a liquid chloride brine reports a more persistent corrosion challenge through the winter season.
Should a fleet do undercoating in-house or hire a mobile service?
Either can work if the surface prep and product choice are right. An in-house application gives a fleet control over scheduling and lets a technician coat a truck between other PM work, but it requires the wash-and-dry step to actually happen first, which is easy to skip under shop time pressure. A mobile or shop-based service typically bundles the wash into the appointment and carries a product-specific application tool, which can be the better option for a smaller fleet without a dedicated undercoating bay.
Truck corrosion prevention works best as a scheduled program, not a reaction to visible rust. A fleet that pairs a regular de-icer-rated washing with a seasonal undercoating, a documented frame inspection, and routine attention to an electrical ground consistently avoids the two outcomes that cost the most — an out-of-service frame violation and an intermittent electrical fault that takes hours to trace back to a corroded connector — the same discipline Michael Nielsen and Heavy Duty Journal's editorial team hold every guide on heavydutyjournal.com to.
Whether a fleet runs five trucks or five hundred, the same four steps apply at the same interval: wash for the chemistry actually on the road, coat before exposure rather than after damage, inspect on a documented schedule, and protect the electrical ground that fails silently.
Send This to Whoever Runs Your PM Schedule
If your shop is still treating undercoating as an occasional extra rather than a seasonal line item, this is the guide that makes the case for changing that before the next winter hits.