By Michael Nielsen, Publisher | 15+ Years in Diesel Repair
Last Updated: September 2026
⏱ Estimated reading time: 15+ minutes
Heavy equipment hydraulic systems deliver the force that powers excavators, loaders, cranes, and dozers across construction sites, mines, and industrial facilities. These fluid-powered systems transform engine power into precise lifting, positioning, and movement capabilities that make modern heavy equipment productive. Michael Nielsen and Heavy Duty Journal's editorial team built this guide because without proper hydraulic maintenance, even the most robust machinery faces costly breakdowns, dangerous failures, and unplanned downtime that halts operations.
Contaminated fluid destroys precision components. Worn seals create dangerous leaks under extreme pressure. Power loss and control failures put operators at risk while stopping productive work. Systematic hydraulic system care delivers measurable returns through extended equipment lifespan, maximized uptime, and avoided emergency repairs that cost far more than routine service.
Key Takeaways
- ✓Contamination causes the large majority of failures: Fluid cleanliness to target ISO 4406 codes prevents most hydraulic component damage.
- ✓Daily inspections prevent costly breakdowns: Systematic pre-operation checks catch problems before they escalate.
- ✓Filter service is critical: Replace filters based on differential pressure readings and contamination analysis, not just hours.
- ✓Proper fluid selection matters: Using manufacturer-specified viscosity grades and fluid types protects seals and components.
- ✓Safety protocols are non-negotiable: Hydraulic injection injuries from high-pressure leaks require immediate emergency treatment.
- ✓Documentation drives improvement: Tracking maintenance data reveals patterns that optimize service intervals and predict failures.
In This Guide
- Understanding Hydraulic Systems in Heavy Equipment
- Essential Tools for Hydraulic System Maintenance
- Hydraulic Fluid Selection and Quality Management
- Daily Pre-Operation Inspection Procedures
- Implementing a Preventive Maintenance Program
- Hydraulic Filter Service and System Flushing
- Servicing Hydraulic Pumps and Cylinders
- Critical Safety Protocols During Hydraulic Maintenance
- Maintenance Documentation and Record Management
- Frequently Asked Questions
Understanding Hydraulic Systems in Heavy Equipment
Hydraulic power transfer allows seamless force transmission, reduced mechanical wear, and instantaneous power amplification within compact spaces. Pascal's principle forms the theoretical foundation: pressure applied to confined fluid transmits equally in all directions throughout the container. When force applies to a small piston, the resulting pressure affects a larger piston with proportionally greater force output.
The system converts mechanical energy to fluid power and back through three stages. First, the pump transforms rotational engine power into fluid flow and pressure. Second, pressurized fluid travels through valves and hoses to reach actuators. Third, cylinders or motors convert fluid energy back into useful mechanical force.
Core Components and Functions
Hydraulic pumps serve as the heart of the system, converting mechanical energy from the engine into fluid pressure. Common pump types include gear pumps for simpler applications, piston pumps for high-pressure systems, and vane pumps offering smooth operation — each with distinct advantages for specific equipment applications.
Cylinders transform fluid pressure back into linear mechanical force, extending and retracting to move equipment attachments, lift loads, and position machinery. Double-acting cylinders apply force in both directions, while single-acting versions rely on external forces for return motion.
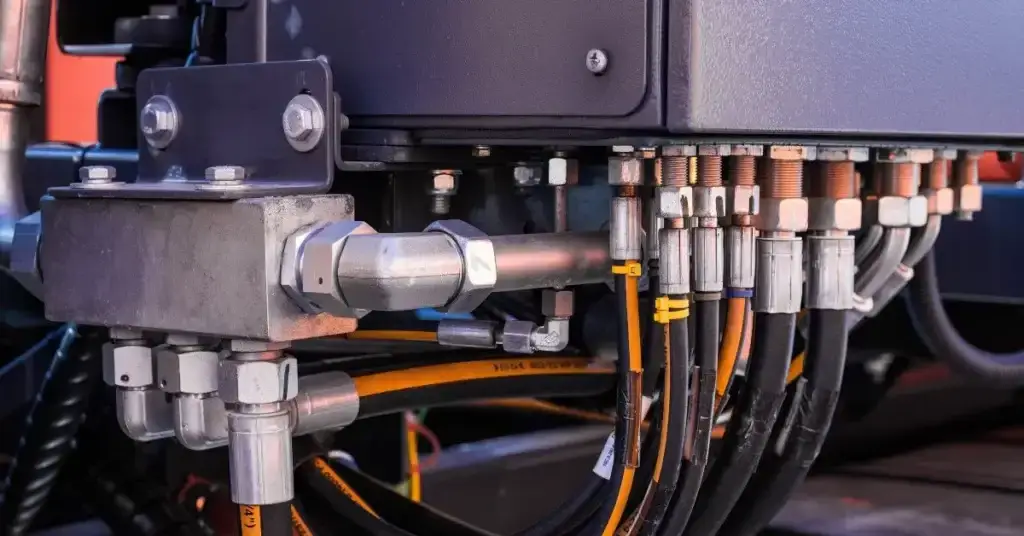
Supporting components include hydraulic motors converting fluid energy into rotational power, control valves directing flow throughout the system, reservoirs storing fluid and dissipating heat, accumulators maintaining pressure stability, and filters removing contamination to protect precision components.
Equipment Types Relying on Hydraulics
Excavators represent the most hydraulic-intensive construction equipment, using multiple cylinders to control boom, stick, bucket, and swing functions simultaneously. Bulldozers employ hydraulic cylinders for blade positioning while hydraulic motors drive tracks. Wheel loaders use hydraulics for bucket positioning and steering control.
Mobile cranes depend on hydraulic systems for boom extension, load lifting, and outrigger stabilization with millimeter-accuracy positioning. Backhoes, forklifts, dump trucks, motor graders, and specialized equipment including concrete pumps and aerial lifts all incorporate hydraulic components for primary operations. HDJ's excavator hydraulic problems guide covers the diagnostic side once a system already shows a fault.
Essential Tools for Hydraulic System Maintenance
Successful hydraulic system servicing depends on precise diagnostic instruments, contamination detection devices, and comprehensive safety gear. Without proper equipment, technicians cannot accurately assess system conditions or protect themselves from hazards inherent in high-pressure fluid systems.
Pressure Testing and Diagnostic Instruments
Pressure gauges provide real-time measurements of system operating pressures at various circuit points, and require annual calibration to maintain accuracy within roughly ±2% of full scale. Flow meters measure fluid volume moving through the system per unit time, helping identify restrictions, pump wear, and component inefficiencies.
Temperature sensors complement pressure readings by revealing thermal patterns indicating friction, contamination, or inadequate cooling. Advanced maintenance facilities employ electronic diagnostic scanners interfacing with equipment control systems to retrieve fault codes, monitor sensor data, and track performance trends.
| Instrument Type | Primary Function | Calibration Frequency |
|---|---|---|
| Hydraulic Pressure Gauge | Measures system pressure at test points | Annually (~±2% accuracy) |
| Flow Meter | Quantifies fluid volume movement | Every 6 months |
| Temperature Sensor | Monitors thermal conditions | Quarterly |
| Diagnostic Scanner | Retrieves fault codes and data | Software updates as released |
Fluid Analysis and Contamination Detection
Particle counters quantify contamination levels according to ISO 4406 cleanliness standards, classifying fluid based on particle size and concentration. Per Machine Design, citing hydraulic component maker Muncie Power Products, up to 90% of all hydraulic system failures can be attributed to contaminated oil. Portable particle counters provide immediate on-site analysis, drawing fluid samples through optical sensors that count and size particles in real time.
Fluid sampling equipment includes specialized bottles, vacuum pumps, and sample ports preventing external contamination during collection. Test kits detect water contamination through chemical reactions and identify fluid degradation by measuring viscosity, acidity, and additive depletion.
Up to 90%
of hydraulic system failures trace back to contaminated fluid, per Machine Design's reporting on data from hydraulic component maker Muncie Power Products.
Required Safety Equipment
Personal protective equipment forms the first line of defense against hydraulic maintenance hazards. Safety glasses with side shields prevent fluid splashes during connection removal or filter changes; face shields provide additional protection during high-pressure testing above roughly 1,500 PSI.
Chemical-resistant gloves made from nitrile or neoprene protect hands from prolonged fluid exposure causing dermatitis. Protective clothing includes fluid-resistant coveralls preventing contamination of personal clothing, and long sleeves are mandatory near pressurized systems to protect against hydraulic fluid injection injuries.
Lockout-tagout devices prevent accidental system energization during maintenance, securing valve handles, electrical disconnects, and control switches — each technician applies their own personal lock ensuring they control when equipment restarts.
Hydraulic Fluid Selection and Quality Management
Selecting the right hydraulic fluid and maintaining its quality determines the longevity and reliability of an entire hydraulic system. This critical component circulates through every pump, valve, cylinder, and hose — poor fluid choices or contaminated oil create cascading problems compromising seals, damaging precision components, and reducing equipment productivity.
Selecting the Correct Fluid Grade
Viscosity grade is the most critical specification, determining how easily fluid flows through system components at different temperatures. Manufacturers specify viscosity grades using ISO standards, typically ranging from ISO VG 32 to ISO VG 68 for most heavy equipment applications. Lower numbers indicate thinner fluids flowing easily in cold conditions; higher numbers represent thicker fluids maintaining protective film strength under heavy loads.
Three primary fluid types dominate the market: mineral-based hydraulic oils offering excellent lubrication and cost-effectiveness, synthetic hydraulic fluids providing superior temperature stability and extended service life, and biodegradable hydraulic fluids minimizing environmental impact near waterways.
Always consult equipment manufacturer specifications before selecting hydraulic fluid — OEM machine fluid recommendations account for pump design, operating pressures, seal materials, and expected temperature range. Using the recommended fluid type and maintaining consistency with the same brand prevents compatibility issues from mixing different additive packages.
Testing Fluid Condition
Visual inspection provides the first line of defense. Contaminated fluid exhibits several visible indicators: cloudy or milky appearance suggesting water contamination, dark discoloration indicating oxidation or thermal breakdown, excessive foaming revealing air entrainment or additive depletion, and unusual odors signaling chemical degradation.
Laboratory fluid analysis provides precise contamination data beyond visual inspection capability, identifying water content, particle counts, additive depletion, and viscosity change. ISO 4406 cleanliness codes classify contamination using three numbers representing particle counts at different size ranges — a target cleanliness level of roughly 15/13/10 represents acceptable conditions for most hydraulic systems, though the specific target should follow the component manufacturer's own specification for the most sensitive parts in the system.
Storage and Contamination Prevention
Contamination prevention begins before hydraulic oil enters equipment. Store fluid in clean, climate-controlled locations away from temperature extremes and moisture sources, in sealed containers that prevent airborne contaminants from entering stored oil.
New fluid arrives from manufacturers with some contamination from production and packaging — never assume new hydraulic fluid meets system cleanliness requirements. Filter new fluid before adding it to machines, using portable filtration carts equipped with appropriate micron ratings.
Contamination enters systems through multiple pathways: worn seals allowing dirt ingestion during cylinder retraction, breather caps without filtration permitting airborne particles into reservoirs, and improper service procedures introducing contaminants during filter changes.
Daily Pre-Operation Inspection Procedures
Every shift begins with critical inspection procedures identifying hydraulic system issues before they cause operational downtime. Consistent inspection habits prevent minor issues from escalating into major system breakdowns, transforming equipment operators into the first line of defense against costly failures.
Systematic Visual Examination
A comprehensive visual inspection follows a methodical pattern covering all hydraulic components systematically. Develop a consistent inspection route examining pumps, motors, cylinders, hoses, fittings, and reservoirs in the same sequence each day, starting at the hydraulic reservoir and working outward through the entire system.
Warning signs requiring immediate attention include hose bulging or soft spots suggesting internal reinforcement failure, loose fittings identified by hand-checking connection tightness, accumulation of dirt on cylinder rods before retraction, damaged protective sleeves on hoses, and component discoloration indicating excessive heat buildup.
Checking Fluid Levels and Condition
Proper fluid level checks require positioning equipment on level ground with hydraulic cylinders fully retracted. Fluid should rest between minimum and maximum marks when the system reaches operating temperature — low fluid levels cause pump cavitation, damaging internal components through rapid bubble formation and collapse.
| Fluid Appearance | Contamination Type | Required Action |
|---|---|---|
| Milky or cloudy | Water contamination | Drain and replace immediately |
| Darkened or black | Oxidation or thermal degradation | Schedule fluid change, investigate heat sources |
| Visible particles | Metal debris or dirt | Filter inspection, possible system flush |
| Foamy or aerated | Air entrainment | Check reservoir level, breather function |
Identifying Leaks and Warning Signs
Effective leak detection combines active leak observation with evidence examination from previous seepage. Fresh leaks appear as wet spots, drips, or spray patterns on components — evidence of previous leaks (dried residue, staining, oil accumulation in component recesses) indicates chronic seepage warranting investigation even when active leaking isn't visible.
Address all identified leaks immediately rather than deferring repair. Small leaks expand rapidly once seal integrity is compromised, and the repair cost stays minimal compared to replacing fluid, cleaning contamination, and repairing secondary damage from prolonged leakage.
Implementing a Preventive Maintenance Program
Proactive hydraulic maintenance scheduling separates high-performing fleets from those plagued by unexpected downtime. A structured preventive maintenance program transforms maintenance activities from urgent responses to planned interventions maximizing equipment reliability.
Weekly Service Tasks
Weekly inspections go beyond daily checks to identify emerging issues before they compromise system performance — detailed visual inspection under varied operating conditions, filter condition assessment monitoring pressure differentials, hydraulic oil sampling establishing trending data, connection tightness verification, and documentation of fluid temperature during operation.
Monthly Maintenance Requirements
Monthly maintenance represents a comprehensive system evaluation assessing overall hydraulic performance — pressure tests across different system functions verifying pumps, valves, and cylinders operate within manufacturer specification, complete fluid analysis providing detailed contamination data including particle counts, water content, and additive depletion.
Replace filters according to manufacturer service interval, or earlier if condition monitoring indicates excessive contamination — monthly intervals work for moderate-duty applications, while severe service may need more frequent replacement.
Quarterly and Annual Overhauls
Major maintenance activities address comprehensive system needs beyond routine tasks. Quarterly maintenance focuses on component-level inspection and replacement based on wear patterns — removing and inspecting high-wear components like pump cartridges, cylinder seals, and control valve spools.
Annual system overhauls include complete fluid replacement removing accumulated contaminants, system flushing eliminating varnish deposits and sludge, seal replacement in cylinders and rotary actuators, pump inspection and rebuild based on hour meters, and detailed performance documentation establishing baselines.
Hydraulic Filter Service and System Flushing
Filter replacement and flushing procedures represent essential preventive maintenance tasks, since contamination remains the primary cause of hydraulic system failure. Regular filter service combined with proper system flushing protects expensive components from premature wear.
Filter Types and Change Intervals
Hydraulic systems employ multiple filter types serving specific contamination control functions. Suction filters protect pumps from large particles in the reservoir, typically featuring coarse mesh elements capturing particles larger than 100 microns, with inspection recommended every 500 operating hours.
Pressure filters install downstream from pumps protecting sensitive control valves and actuators from fine contamination, capturing particles as small as 3–10 microns with change intervals of 1,000–2,000 hours. Return line filters provide final contamination control before fluid re-enters the reservoir, removing wear particles generated during operation.
Free Diesel Maintenance Checklist
Get HDJ's free, field-tested diesel maintenance checklist delivered instantly to your inbox — print it, laminate it, keep it in the shop.
Instant PDF • 100% Free • No Spam
Step-by-Step Filter Replacement
Proper filter replacement requires systematic procedures preventing new contamination introduction during service. Begin with complete system shutdown, lockout-tagout engagement, and pressure release through cycling control functions or opening bleed valves — verify zero pressure using calibrated gauges before proceeding.
Clean external filter housing thoroughly before opening to prevent dirt entering the system. Position a drain pan beneath housing, remove the bowl carefully, and extract the used filter into a sealed disposal container. Inspect the bowl interior for accumulated sludge or metal particles indicating component wear.
Verify the replacement filter matches manufacturer specification. Pre-fill the new element with clean hydraulic fluid to prevent pump cavitation during startup. Install according to directional flow arrows, replace all O-rings with new components, and tighten the bowl to manufacturer torque specification.
Complete System Flushing
Simply changing filters doesn't thoroughly clean a contaminated system. System flushing removes embedded contamination from internal passages, component surfaces, and reservoir walls — a comprehensive cleaning that becomes necessary before installing new major components or addressing persistent contamination issues.
Effective flushing requires proper velocities creating turbulent flow that dislodges embedded particles — target flow velocities of roughly 10–15 feet per second through system lines to mobilize contaminants without damaging components. Circulate heated flushing fluid (roughly 140–160°F) while monitoring contamination levels with particle counters until counts consistently meet the target ISO cleanliness code.
Servicing Hydraulic Pumps and Cylinders
Pumps and cylinders serve as primary actuating components transforming pressurized fluid into productive work. These critical elements experience significant stress during operation, making them vulnerable to wear that needs a specialized maintenance approach.
Monitoring Pump Performance
Establish baseline performance metrics when equipment is new or after pump replacement, documenting pressure output, flow rate, operating temperature, and sound level. Regular pressure verification using calibrated gauges identifies declining pump efficiency before complete failure — a 10% reduction in flow rate typically indicates significant internal wear requiring overhaul or replacement.
Temperature monitoring reveals internal wear and excessive friction within pump assemblies — operating temperature exceeding normal ranges by 20°F or more indicates a potential problem. Unusual noises signal developing issues too: whining suggests cavitation, knocking indicates loose components or bearing failure, and grinding points to contamination damage.
Cylinder Seal Inspection and Replacement
Visual inspection of cylinder rods provides the first line of defense against seal failure. Examine the entire rod surface for corrosion, pitting, and scoring that damages seals through excessive friction. External fluid seepage around rod seals needs immediate attention, while reduced cylinder performance and position drift under load signal internal seal deterioration.
⚠️ Safety Warning
Always depressurize cylinders completely and engage lockout-tagout procedures before seal replacement. Residual pressure can cause violent component ejection during disassembly. Verify zero pressure at multiple test points before beginning work.
Seal replacement requires careful attention to component orientation, torque specification, and cleanliness. Mark cap and tube alignment before separation, clean seal grooves thoroughly, lubricate new seals with system fluid before installation, and follow the recommended tightening sequence to distribute clamping forces evenly.
Cavitation and Aeration Prevention
Low fluid level is the leading cause of cavitation in hydraulic pumps — insufficient fluid allows pumps to draw air, forming bubbles that collapse violently inside the pump and erode metal surfaces. Restricted suction lines from undersized hoses, clogged inlet strainers, or excessive line length prevent adequate fluid flow, creating vacuum conditions that promote cavitation.
Aeration introduces air through external sources rather than vapor formation — loose suction line connections, damaged pump shaft seals, and low fluid levels all allow atmospheric air entry, creating foam in the reservoir. Prevention means maintaining proper fluid levels, sizing reservoirs appropriately for air separation, specifying adequate suction line diameter, and regularly inspecting suction components for air infiltration.
Critical Safety Protocols During Hydraulic Maintenance
Hydraulic maintenance presents unique hazards requiring comprehensive safety protocols to prevent severe injuries and fatalities. OSHA's guidance on controlling hazardous energy specifically addresses hydraulic, pneumatic, and other stored energy sources that can cause harm during servicing. These systems operate under pressures exceeding 3,000 PSI, creating risks demanding respect and careful attention — every technician performing maintenance must be competent, well-trained, and fully aware of the dangers involved.
Depressurization and Lockout-Tagout
Residual pressure can remain trapped in hydraulic systems even after equipment shutdown. The first step is identifying all pressure sources including accumulators, cylinders, and line sections containing trapped fluid, then slowly releasing trapped pressure through appropriate relief valves — never rushing the process, since rapid release can cause component failure or fluid spray.
Before opening any connection, verify zero pressure using pressure gauges at multiple test points. Implement complete lockout-tagout procedure per OSHA standard 29 CFR 1910.147, placing physical locks on energy isolation devices with identification tags — each technician working on the equipment places their own personal lock, ensuring they control restart timing.
Fluid Handling Safety
Hydraulic fluids pose multiple health and environmental hazards depending on chemical composition. Always wear appropriate PPE: chemical-resistant gloves protecting hands, safety glasses or face shields preventing eye contact, and long-sleeved protective clothing providing a splash barrier.
If hydraulic fluid contacts skin, wash immediately with soap and water — never use solvents or harsh cleaners, which drive contaminants deeper into tissue. Proper spill cleanup using absorbent materials designed for petroleum products prevents environmental contamination and slip hazards.
Critical Safety Rule
Never use your hands to check for hydraulic leaks. High-pressure fluid streams from pinhole leaks can penetrate skin like hypodermic needles at pressures above 100 PSI. Use cardboard or paper to detect fluid spray from suspected leak points.
Understanding Hydraulic Injection Injuries
Hydraulic injection injuries occur when high-pressure fluid penetrates skin and underlying tissue, often through nearly invisible pinhole leaks. Per UK Health and Safety Executive guidance, the small entry wound makes these injuries look minor, but they are true medical emergencies requiring immediate treatment.
Pressure above 100 PSI can break the skin barrier, and most hydraulic systems operate well above that. Injected fluid spreads through tissue planes causing extensive internal damage not immediately apparent. Medical literature indexed in NIH's PMC documents amputation rates in a meaningful range for these injuries, with delayed treatment significantly worsening outcomes. If an injection injury occurs, seek emergency medical treatment immediately regardless of how the wound looks.
Inform emergency personnel the injury involves pressurized hydraulic fluid injection and provide the safety data sheet for the specific fluid. Early surgical intervention is often necessary to remove contaminated tissue — delay significantly worsens outcomes and increases amputation likelihood.
Maintenance Documentation and Record Management
Documentation transforms routine maintenance from reactive tasks into strategic asset management. Comprehensive records enable operators to identify patterns, predict failures, and make informed decisions about equipment lifecycle management, while demonstrating equipment care that increases resale value.
Critical Information for Service Logs
Every maintenance entry should document: date and time with start and completion timestamps, equipment identification including make, model, and serial number, operating hours at service time, specific tasks performed with detailed descriptions, components replaced with part numbers and quantities, fluid added or changed with type and volume, test results including pressure readings and temperature data, abnormalities observed, technician identification, and next scheduled service date.
Tracking Component Service Life
Component tracking establishes predictable replacement schedules preventing unexpected failure. Priority components for lifecycle monitoring include hydraulic filters with installation dates, hoses noting manufacture date and replacement history, seals in cylinders and pumps, pump assemblies with performance metrics, and control valves with response characteristics.
Tracking enables predictive replacement before failure occurs and identifies components with abnormally short service lives — premature failures often indicate a system problem (contamination, excessive pressure, improper installation) rather than a component quality issue.
Digital Maintenance Management
Computerized maintenance management systems automate documentation, providing capability impossible with paper records: automated service reminders based on calendar date or hours, parts inventory tracking with reorder notification, mobile access for field technicians enabling real-time data entry, performance analytics and trend reports, and digital work order generation with task checklists.
Digital systems eliminate lost-record risk, enable simultaneous access from multiple locations, and cut documentation time meaningfully compared to manual methods. Trend analysis capability identifies patterns across an entire equipment fleet that would be invisible in paper records. HDJ's heavy equipment mechanic tools guide covers the physical toolkit side of the shop this documentation supports.
Frequently Asked Questions
How often should hydraulic fluid be changed in heavy equipment?
It depends on operating conditions, equipment type, and fluid analysis results. Most manufacturers recommend replacement every 2,000–4,000 operating hours under normal conditions; severe duty with high temperature, dusty environments, or continuous operation may call for changes every 1,000–2,000 hours. Regular quarterly fluid analysis testing — revealing contamination level, additive depletion, and viscosity change — is the most reliable way to determine actual change timing rather than an arbitrary schedule.
What causes most hydraulic system failures?
Fluid contamination causes the large majority of hydraulic system failures — particulate matter like dirt and metal particles, water intrusion, and air entrainment all damage precision components, accelerate wear on pumps and valves, degrade seals, and compromise system efficiency. Prevention requires proper filtration, clean fluid handling procedure, sealed reservoir maintenance, and regular fluid analysis detecting contamination before it causes component damage.
What are signs of a failing hydraulic pump?
Unusual whining or grinding noise during operation, elevated fluid temperature beyond a normal 120–140°F range, slow or erratic cylinder movement, reduced lifting capacity, and visible fluid foaming in the reservoir. Whining specifically indicates cavitation from air in the system or restricted suction flow. Any of these symptoms warrant immediate inspection to prevent catastrophic failure and secondary damage to other components.
How do you check hydraulic fluid condition?
Visual inspection gives an initial assessment: clean fluid maintains consistent color and transparency, milky appearance indicates water contamination, dark discoloration suggests oxidation, and excessive foaming reveals air entrainment. Professional laboratory analysis measures particle counts per ISO 4406 standards, water content, viscosity change, and additive depletion for accurate condition assessment — portable particle counters provide on-site contamination data in between lab tests.
What safety precautions are essential for hydraulic maintenance?
Complete system depressurization before disconnecting components, proper lockout-tagout procedure preventing accidental energization, and PPE including safety glasses, chemical-resistant gloves, and face shields for high-pressure work. Never use your hands to check for leaks, since high-pressure fluid can cause a hydraulic injection injury requiring emergency treatment. Keep spill containment materials and emergency eyewash stations accessible near work areas.
Protect Your Equipment Investment Through Systematic Care
Heavy equipment hydraulic maintenance represents a critical investment delivering measurable return in operational performance and cost control. The systematic approach in this guide — from daily inspection through comprehensive service programs and accurate documentation — works as a unified system protecting equipment value while maximizing productive uptime.
Organizations committing to these protocols achieve superior equipment reliability compared to those treating hydraulic service as optional. The benefit extends beyond avoiding breakdowns to include reduced repair expense, minimized production interruption, and enhanced workplace safety — the same discipline Michael Nielsen and Heavy Duty Journal's editorial team hold every guide on heavydutyjournal.com to.
Share This Maintenance Guide
Know a fleet manager or maintenance supervisor who could benefit from these hydraulic system care strategies? Share this guide with your professional network.