By Michael Nielsen, Publisher | 15+ Years in Diesel Repair
Last Updated: October 2026
Diesel shop compressed air quality is a maintenance category of its own. Walk into most diesel shops and you will see good impact wrenches, air ratchets, and spray equipment in every bay. What you will not see is the air running through them, and in many shops that air is quietly damaging every tool it touches.
Moisture, oil carryover, and airborne particles are constant byproducts of shop air compression. Without treatment matched to the job, those contaminants travel into tool internals, air lines, and spray equipment. This Heavy Duty Journal guide covers what the contaminants do, how to treat air in stages, and what to check and when.
Key Takeaways
- ✓Air quality, not just pressure, drives tool life. Moisture, oil, and particles leave the compressor with the air and end up inside tools and spray equipment.
- ✓Treat air in stages. Drain and cool, dry, then filter at the point of use, instead of relying on one filter.
- ✓Match air quality to the end use. DOE notes that overtreating air beyond what the end use needs wastes money and energy.
- ✓Leaks waste a lot of air. DOE says leaks often waste as much as 20-30% of a compressor's output.
- ✓Measure pressure at the tool. Low pressure at the farthest drop is often a distribution or filter problem, not a compressor problem.
In This Guide
- Diesel Shop Compressed Air Quality: Why It Matters
- The Hidden Costs of Contaminated Shop Air
- Moisture, Oil, and Particles: The Contaminants to Control
- Treating Shop Air in Stages: Dryers, Filters, and Drains
- Sizing the System and Watching Pressure Drop
- Keeping Diesel Shop Compressed Air Quality Up: What to Check and When
- Frequently Asked Questions
- The Bottom Line
Diesel Shop Compressed Air Quality: Why It Matters
Compressed air is one of the most widely used utilities in a diesel service environment. Air-powered impact wrenches generate the torque needed to remove seized wheel fasteners. Air ratchets speed up routine disassembly.
Air chisels, die grinders, and blow guns handle tasks that electric tools can't match for convenience in a busy bay. The compressor running in the corner of the shop is easy to take for granted — right up until the tools start failing, the paint job develops fisheye defects, or an impact wrench loses its snap midway through a brake job.
The root of most of those problems isn't tool age or brand — it's air quality. A compressor pulls in ambient shop air, which contains humidity, dust, and in some environments, chemical vapors. Compression concentrates all of those contaminants. Without deliberate treatment at multiple stages, everything downstream — every tool, every line, every fitting — receives contaminated air on every cycle.
The Hidden Costs of Contaminated Shop Air
The damage from poor compressed air quality accumulates in ways that rarely get attributed to the correct cause. A die grinder that starts feeling sluggish gets replaced rather than traced back to a saturated filter reducing supply pressure. An impact wrench that drops torque output gets blamed on wear rather than moisture rust building up on the internal vanes. Paint rework gets logged as a product or technique problem rather than a water contamination issue at the gun.
The cumulative costs are significant. Moisture corrodes the precision internal components of rotary air tools — vane-type motors are particularly vulnerable because the vanes must seat tightly against the rotor housing to maintain pressure differential. As moisture introduces rust, those tolerances open up, power drops, and air consumption rises. Oil carryover contaminates spray equipment, requiring additional cleaning time and causing adhesion failures in coatings. Particulate from degraded pipe or aging lines scores internal tool passages and accelerates wear across every fitting and coupler in the system.
20-30%
Share of a compressor's output that leaks often waste, per the U.S. Department of Energy's Minimize Compressed Air Leaks tip sheet.
Leaks add to the problem. DOE notes that leaks cause fluctuating system pressure, which makes air tools function less efficiently, and that they force the compressor to run more. The most common leak points are couplings, hoses, fittings, quick disconnects, filter-regulator units, and condensate traps, which describes most of what hangs in a diesel bay.
Moisture, Oil, and Particles: The Contaminants to Control
Moisture is the most common and most damaging contaminant in shop air systems. Ambient air contains water vapor — how much depends on temperature and relative humidity. When that air is compressed to typical shop pressures of 90–120 PSI, the water vapor concentration increases proportionally. As the compressed air cools in distribution lines, that vapor condenses into liquid water that pools in low points, collects in filter bowls, and enters tool air inlets with every trigger pull.
Oil carryover is the second major threat. Oil-lubricated compressors, including many piston-type shop units, use oil in the compression chamber, and despite rings and separator elements some oil vapor and aerosol passes into the air stream. Over a full shift of tool use, that oil collects in air lines, tool inlets, and spray gun passages.
The ISO 8573-1:2010 standard specifies purity classes for compressed air in terms of particles, water, and oil. A purity requirement is written by listing the class for each contaminant, so a spec reads as three numbers. As of October 2026, ISO lists the 2010 edition as current, with a revision under development. The standard defines the classes but does not say which class a given tool needs. That comes from the tool, spray equipment, or coating maker.
As a reference, the table shows selected water and oil classes. Class 2 water is a pressure dew point of -40°C, which is also -40°F, and Class 2 oil is 0.1 mg/m³ or less. The values come from published summaries of the standard, which is sold by ISO, so confirm against the standard before you write a spec.
| ISO 8573-1:2010 class | Pressure dew point (water) | Oil content |
|---|---|---|
| Class 1 | -70°C (-94°F) or lower | 0.01 mg/m³ or less |
| Class 2 | -40°C (-40°F) or lower | 0.1 mg/m³ or less |
| Class 3 | -20°C (-4°F) or lower | 1 mg/m³ or less |
| Class 4 | +3°C (37°F) or lower | 5 mg/m³ or less |
DOE's guidance makes the practical point: air quality is set by the dryness and contaminant level the end uses require, and treating air beyond what the end use needs wastes money and energy. See DOE's Compressed Air Tip Sheet #4. Impact tools and grinders have different needs than a spray gun, so treat the main line for the general case and add treatment at the drops that need more.
Safety matters too. OSHA 29 CFR 1910.242(b) allows compressed air for cleaning only when it is reduced to less than 30 psi, and then only with effective chip guarding and personal protective equipment. See the OSHA standard. Never point air at skin, and depressurize line couplers before disconnecting them. HDJ's PPE guide covers eye and hearing protection.
Treating Shop Air in Stages: Dryers, Filters, and Drains
Treating compressed air effectively requires a staged approach. No single component handles moisture, oil, and particulate across all conditions. A properly specified system addresses each threat at the right point in the distribution chain.
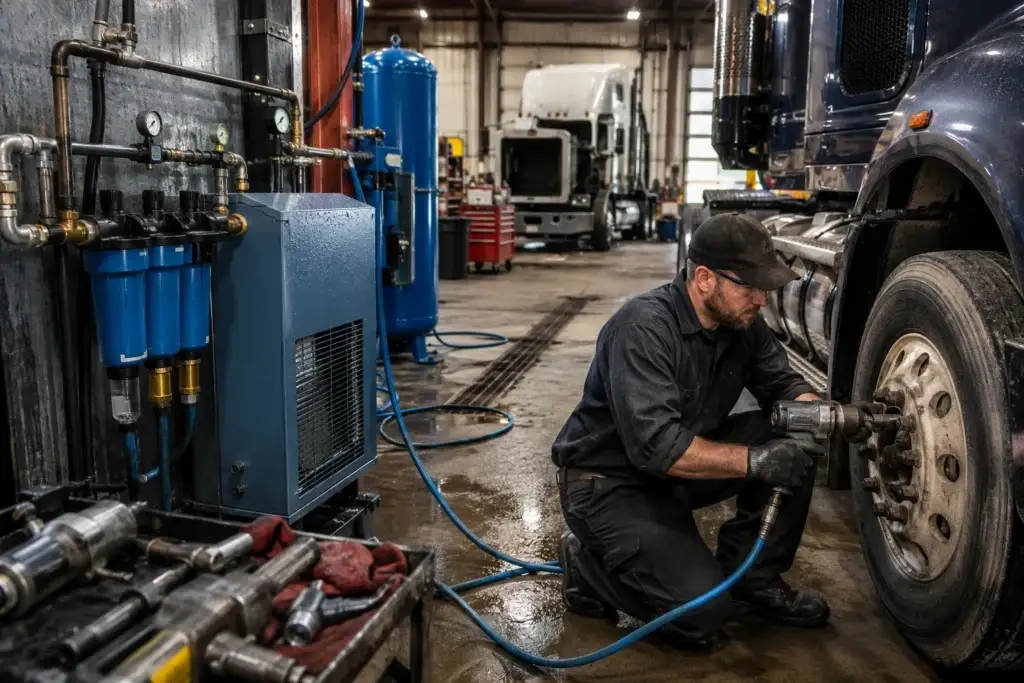
The first stage is cooling and draining. Hot air straight from the compressor carries its moisture as vapor, and cooling it lets bulk water condense where a drain can remove it. Check whether your compressor has an aftercooler, since smaller units may have little aftercooling, and make sure the receiver tank and low points have working drains.
The second stage is a dedicated air dryer. A refrigerated dryer typically delivers a pressure dew point near 37°F (3°C), which fits ISO water Class 4 in the table above. That is often enough for general tool air in a heated shop. Shops that spray paint, or that run air lines through unheated spaces in cold climates, may need a desiccant dryer, which can reach -40°F or lower but has more maintenance and operating cost.
The third stage is point-of-use filtration at the drops that need it. A coalescing filter removes oil aerosol and fine particles. A spray drop may add an activated carbon stage downstream to remove oil vapor, if the spray equipment maker calls for it. Size filters for the flow they will see, since an undersized filter adds pressure drop and starves tools.
Equipment selection should follow from your measured needs, not from a catalog. HDJ's commercial diesel shop equipment list covers the broader bay equipment picture, including air supply.

Sizing the System and Watching Pressure Drop
Air quality problems are compounded by undersized or restricted systems. When pressure at the tool drops under load, tools run below rated speed, generate more heat, and put more stress on internal parts. Moisture and oil then speed the wear that thermal stress causes.
Size by the load, not by the biggest tool. DOE's guidance says the required volume comes from summing the requirements of your applications while accounting for load factors and duration. The total is not the sum of the maximum needs of each tool, but the sum of the average air consumption of each.
Here is an example with assumed numbers. A 3/4-inch impact wrench rated at 8 CFM used 20% of the time, a 1/2-inch air ratchet at 5 CFM used 15% of the time, and a die grinder at 5 CFM used 30% of the time average 3.85 CFM, against 18 CFM if all three ran flat out together. Read each tool's rated consumption from its manual, and ask a compressed air specialist how much storage you need for the peaks.
Pressure drop is the reduction in pressure from the compressor discharge to the point of use, and it occurs as air passes through treatment and distribution. DOE notes that low or fluctuating pressure at end uses is too often misdiagnosed as not enough discharge pressure. A pressure profile, which is a series of pressure readings at different points in the system, shows which component is causing the drop.
Keeping Diesel Shop Compressed Air Quality Up: What to Check and When
An air system that was correctly specified at installation will slide in quality if maintenance is neglected. Filter elements saturate, dryer performance falls as desiccant exhausts or the refrigerant system loses efficiency, and drain valves stick open or closed. Follow the manufacturer's schedule for each component, and use this as a baseline for the air treatment items.
Daily: Open manual condensate drains at the compressor, receiver tank, and low-point drain legs. Check that automatic drains are cycling. Note operating pressure at the compressor and at the farthest drop under load.
Weekly: Check point-of-use filter bowls for liquid or contamination. Confirm automatic drains discharge cleanly, and check the dryer status indicator if it has one.
Free Diesel Maintenance Checklist
Get HDJ's free, field-tested diesel maintenance checklist delivered instantly to your inbox — print it, laminate it, keep it in the shop.
Instant PDF • 100% Free • No Spam
Monthly: Check the pressure differential across each filter and compare it with the maker's limit. Check compressor oil level and condition, and check desiccant indicators on desiccant dryers.
Annually, or per the maker: Replace filter elements, service desiccant or refrigerated dryer components, and inspect lines and fittings for corrosion, leaks, or damage. Put these items on the shop's PM calendar next to oil changes and safety inspections.
HDJ's air compressor maintenance schedule guide covers the compressor itself, and its air tool care schedule guide covers the tools that sit at the end of the line.
Key Recommendation
Schedule a leak walk-through once a year, with an ultrasonic detector or soapy water, and fix the largest leaks first. Check couplers, hoses, quick disconnects, filter regulators, and drain traps, since DOE lists those as the common trouble spots.
Frequently Asked Questions
What causes moisture in a diesel shop's compressed air?
Compression concentrates water vapor from ambient air. As the air cools in lines and at connections, the vapor condenses into liquid water. High humidity, limited cooling, a missing or undersized dryer, and neglected drains all increase the water that reaches your tools.
How often should compressed air filters be replaced?
Follow the filter maker's schedule and its pressure-differential limit, and check the differential monthly. Many shops also replace elements at least yearly regardless. Drain point-of-use bowls daily, or check automatic drains weekly, so liquid does not carry through.
What type of air dryer does a diesel shop need?
A refrigerated dryer typically gives a dew point near 37°F, which suits general tool air in a heated shop. Spray painting or air lines in unheated or cold spaces may need a desiccant dryer, which can reach -40°F or lower. Check your coating and tool requirements first.
Can contaminated shop air harm air brake components during service?
It can, if shop air is used to charge or test brake systems. Moisture and oil can enter valves and chambers, and residual water can freeze in cold weather. Use clean, dry air for brake work and purge the line before connecting. See HDJ's air dryer guide.
How does diesel shop compressed air quality affect spray painting?
Check the spray equipment and coating maker's requirement first. For reference, ISO 8573-1:2010 Class 2 means oil of 0.1 mg/m³ or less and a pressure dew point of -40°C or lower. Meeting that usually takes a desiccant dryer plus coalescing and carbon filtration at the drop.
The Bottom Line
Diesel shop compressed air quality comes down to treating air in stages, matching treatment to the end use, and checking the system on a schedule. Moisture, oil, and particles are constant outputs of compression, and the only question is whether they are removed before they reach your tools and paint work.
Heavy Duty Journal's guidance at heavydutyjournal.com, from publisher Michael Nielsen and the HDJ editorial team, is to start by draining and measuring pressure at the farthest drop, then add dryer and filter capacity where a tool or coating needs it.
As of October 2026, standards and equipment specifications change, so confirm current figures with your equipment makers before relying on them.
Share This With Your Shop Team
Pass it to your service manager or lead tech before the next tool replacement cycle.